Define the performance envelope
Review minimum breaking load, elongation at break, retained tension where relevant, splitting or tear requirements, and joint performance. State the test method and conditions so results are comparable.
The right specification connects the strap, the equipment and the load.
Explore this capability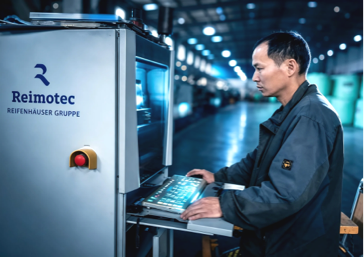
Will the proposed strap meet the demands of our load?
A material name or a breaking-strength figure is only a starting point. Define the complete load, contact surfaces, handling sequence and joining method before approving a PET grade. Newton's Eco, Plus, Ultra and Ultra Max families provide different starting points for that discussion; suitability is established for the proposed specification and application.
Review minimum breaking load, elongation at break, retained tension where relevant, splitting or tear requirements, and joint performance. State the test method and conditions so results are comparable.
Newton integrates Reimotec production technology. Extrusion, drawing, stabilization and winding provide manufacturing context; equipment capabilities alone do not establish the properties of an ordered grade.
Consider corners, protective interfaces, load movement, storage and transport. Agree package-trial criteria alongside strap tests, especially where failure could create a handling risk.
Will it feed, tension and join on our existing equipment?
Newton PET strapping is designed for virtually all common PET-compatible equipment, including hand tools, battery-powered tools, semi-automatic machines and fully automatic lines. The selected grade still needs to match the machine's documented operating range and be checked on the actual setup.
Confirm width, thickness and tolerances, surface, camber, winding, core interface and coil dimensions. A strap that meets a breaking-load requirement may still feed poorly if its format does not fit the line.
Share the machine or tool make and model, joining method, tension range and relevant settings. Follow the equipment manufacturer's instructions and record the setup used during the trial.
Check feeding, tracking, tensioning, joint formation and package condition during representative operation. Equipment limited to PP or steel needs separate manufacturer confirmation before a material change.
Will the next batch behave like the batch we approved?
Consistency begins with an agreed reference. Connect the approved specification and sample decision to dimensional checks, mechanical testing, coil inspection and batch identity. This gives purchasing, production and quality teams a common basis for reviewing repeat supply.
Review width, thickness, tolerances, measured grams per meter, breaking load, elongation, camber, meters per coil, colour and surface against the ordered grade. Define acceptance limits rather than treating nominal dimensions as limits.
The production overview assigns checks to operators, quality testing and release teams. Agree which inspection records and documents accompany the order and how batch labels connect to them.
Confirm the specification revision for repeat orders and agree communication for changes that affect the approved product or process. Review a changed grade or setup before treating it as equivalent.
Share the application, equipment, purchasing volume and questions your team needs answered.
Discuss your requirements